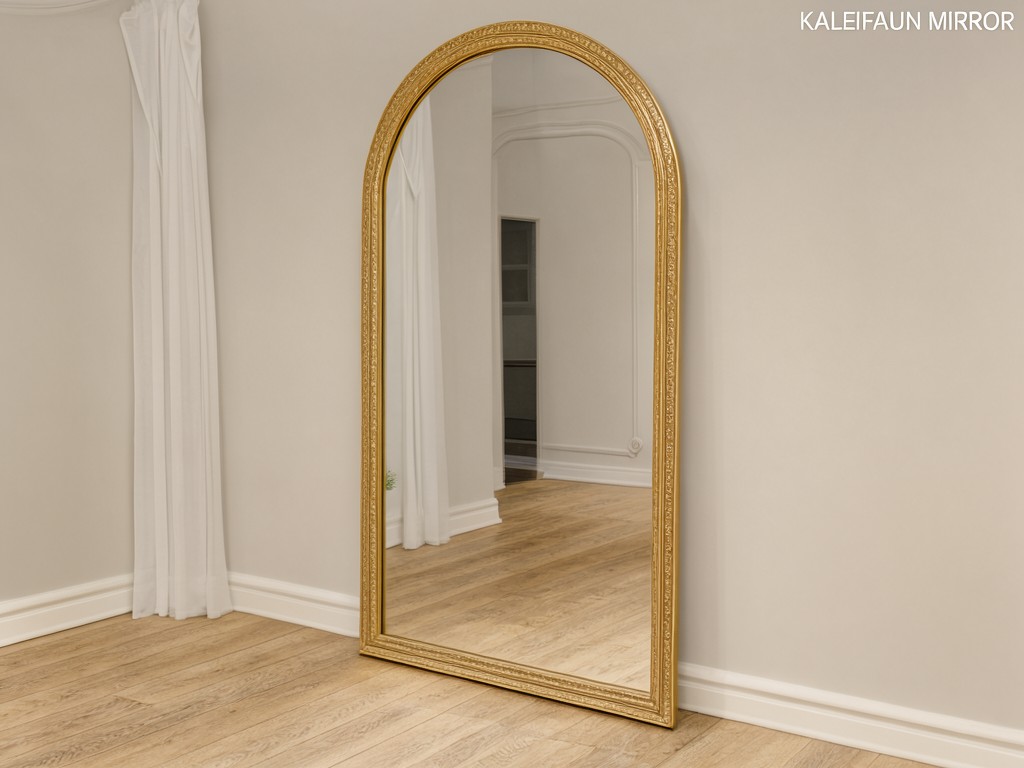
Custom large arched vanity mirror factory: What Buyers Should Check Before Ordering
First-article tooling determines whether the arch profile, edge finish and mounting points match the approved drawing before repeat production starts. For a large vanity mirror, that first article is usually checked against a CNC cutting file and an assembly fixture, not a costly full-size mould.
What Actually Determines Performance
Mirror clarity depends on the glass surface and reflective coating; service life in a bathroom also depends on how well the cut edge and backing resist moisture. A protective backing film can help retain fragments if the glass breaks, but it does not make the mirror unbreakable or replace a required safety-glazing specification.
Glass Build
4 mm glass can reduce weight and cost; 5 mm adds stiffness and mass for larger formats. Confirm the choice against finished dimensions and mounting method.
Arch Geometry
The radius, shoulder transition and overall height define the look. Approve a dimensioned drawing before cutting so revisions do not reach the production batch.
Edge and Backing
Polished exposed edges suit frameless designs. A frame can shield the perimeter, but its finish and joints need their own checks.
Construction Method and Its Effect on Consistency
Process choice shows up later as variation in arch symmetry, polished-edge width and frame fit. A typical sequence starts with mirror-sheet inspection, followed by CNC profile cutting, edge grinding or polishing, backing inspection and frame or bracket assembly. A saved cutting program supports repeat dimensions; a fixture controls bracket position during assembly.
For a framed model, the curved rail may need a dedicated forming setup and a first-article check against the glass profile. That setup adds cost at low volume, while repeat orders spread the fixture and programming expense across more units. Confirm whether a drawing change resets the approved profile or only updates a mounting detail.
Drawing control: Set the overall height, width, arch radius, glass thickness, edge treatment and bracket locations on one approved revision. A stated overall-dimension tolerance, often around ±2–3 mm by agreement, gives inspection a usable pass/fail basis.
Measured Performance in Real Use
Consistency is set at the forming stage and confirmed at final inspection. Buyers should assess reflection distortion across the usable area, visible coating defects, edge quality, and whether the mirror sits flat after mounting. In humid bathrooms, exposed or poorly protected edges are a common starting point for backing deterioration.
Large-format weight rises with glass area and thickness, so the selected wall fixings must suit the mirror and the installation surface. The factory can verify mirror weight and bracket position; the installer must confirm the wall substrate and fixing capacity.
Comparing Two Standard Configurations
The following examples show how construction choices affect quoted cost and handling. Dimensions are common custom-order starting points, not fixed catalogue limits; confirm the final size and weight on the approved specification.
| Parameter | Frameless, Polished Edge | Slim Metal Frame |
|---|---|---|
| Example size | 600 × 1600 mm | 700 × 1700 mm |
| Glass and indicative glass-only weight | 4 mm mirror glass; about 9.6 kg before brackets or backing film | 5 mm mirror glass; about 14.9 kg before frame or brackets |
| Construction trade-off | Lower material cost and a clean perimeter; exposed edge finish needs close control. | Frame adds material and forming work; it covers the edge and sets a defined finish around the arch. |
| Typical material choices | Silvered float glass, polished edge, optional backing film | Silvered float glass with formed metal frame; specify frame alloy and finish for quotation |
Glass-only weights use an approximate glass density of 2,500 kg/m³ and exclude the arch cutout, frame, backing and fittings. Request a finished-unit weight after the exact drawing and material build are set.
What Gets Checked Before Shipment
Inspection should follow the approved sample and drawing, rather than a visual check alone. A practical batch plan can include:
- Measure overall width and height, then compare arch symmetry and bracket locations with the drawing.
- View the reflective surface under consistent lighting for distortion, scratches, spots or coating blemishes.
- Check polished edges for chips and uneven finish; inspect frame joints, finish coverage and fit where applicable.
- Record sample approval, production lot and inspection findings against the buyer’s SKU or purchase order.
Agree the inspection criteria and any required safety-glazing documentation before production. The backing film, if selected, should be recorded as a construction feature rather than treated as proof of a particular safety classification.
Volume Planning and Lead Time
Unit cost usually falls when repeat volume shares the same glass size, arch profile and frame finish. Each added size or finish can create separate material planning, setup and inspection work, so a broad SKU mix may cost more per mirror than a deeper run of one approved configuration.
| Order Stage | MOQ Basis | Planning Lead Time |
|---|---|---|
| Sample and first article | One approved configuration; sample charges may include setup and special handling. | Often 2–4 weeks after drawing and material confirmation. |
| Pilot or first production run | Quoted by size, frame finish and production setup; mixed SKUs may carry separate minimums. | Often 4–8 weeks after sample approval and order confirmation. |
| Repeat order | Higher quantities of an unchanged specification generally improve material utilization and unit pricing. | Set against material availability, line capacity and the confirmed production slot. |
These are planning ranges, not shipment commitments. To protect a retail launch date, include drawing approval, sample review and any finish approval in the purchase schedule; a late specification change can reset the production slot.
Ordering, Tooling and Lead-Time Questions
What should be included in a first-article request?
Send a dimensioned drawing with glass thickness, arch profile, edge finish, frame material and finish, bracket positions, and any backing-film requirement. A reference sample or marked-up image can help resolve appearance details, but it should not replace controlled dimensions.
Does each size need separate tooling?
CNC cutting usually relies on a size-specific program rather than a cutting die. A formed metal frame may need a profile fixture or forming setup, so confirm any setup charge when adding a new arch or frame section.
How can buyers limit lead-time risk across several SKUs?
Approve one specification per SKU before the production slot is booked, and keep changes to size, coating or frame finish out of the order after approval. Ask the factory to confirm material availability and MOQ by configuration rather than treating the full assortment as one interchangeable batch.
Request a Sample Before the Production Slot
Share your target dimensions, order quantity, finish choices and required delivery window. A reviewed first article can settle the arch profile and mounting details before repeat volume is scheduled.